A failed bearing on a transfer conveyor, an air leak in a pneumatic conveying system, or a drifting load cell can stop far more than one machine. In a connected production environment, predictive maintenance for process lines helps manufacturers identify developing equipment issues before they become lost batches, missed shipments, cleanup events, or quality investigations.
For process manufacturers, the objective is not simply to prevent a motor failure. It is to protect the operating window that delivers the required product. That requires maintenance decisions to account for material behavior, process conditions, control performance, sanitation requirements, and the constraints created by upstream and downstream equipment.
Why Process Lines Need a Different Maintenance Strategy
Traditional preventive maintenance is built around time or operating hours. Grease a bearing every six months. Replace a belt after a set number of cycles. Inspect a gearbox during the annual shutdown. This approach remains necessary, particularly for safety-critical components and regulated maintenance activities. But a calendar cannot reveal whether a component is operating under unusual load, degrading early, or performing normally well beyond its assumed replacement interval.
Process lines add another complication: equipment condition and product condition are often linked. A worn rotor in a mill can change particle-size distribution. An agitator seal beginning to fail can introduce contamination risk or alter a vacuum process. A feeder that is losing repeatability can affect formulation accuracy before it triggers a maintenance alarm. The earliest sign of trouble may appear in batch records, energy consumption, motor current, pressure stability, or quality results rather than in a visible mechanical failure.
Predictive maintenance uses condition data to make maintenance work more deliberate. Instead of asking, “When was this component last serviced?” the better question is, “What is this asset telling us about its remaining operating margin, and what will be affected if it degrades further?”
Start With the Critical Process, Not the Sensor
Many predictive maintenance programs stall because the starting point is a technology purchase rather than a production-risk assessment. Adding vibration sensors to every motor may create data, but it does not automatically create a maintenance strategy.
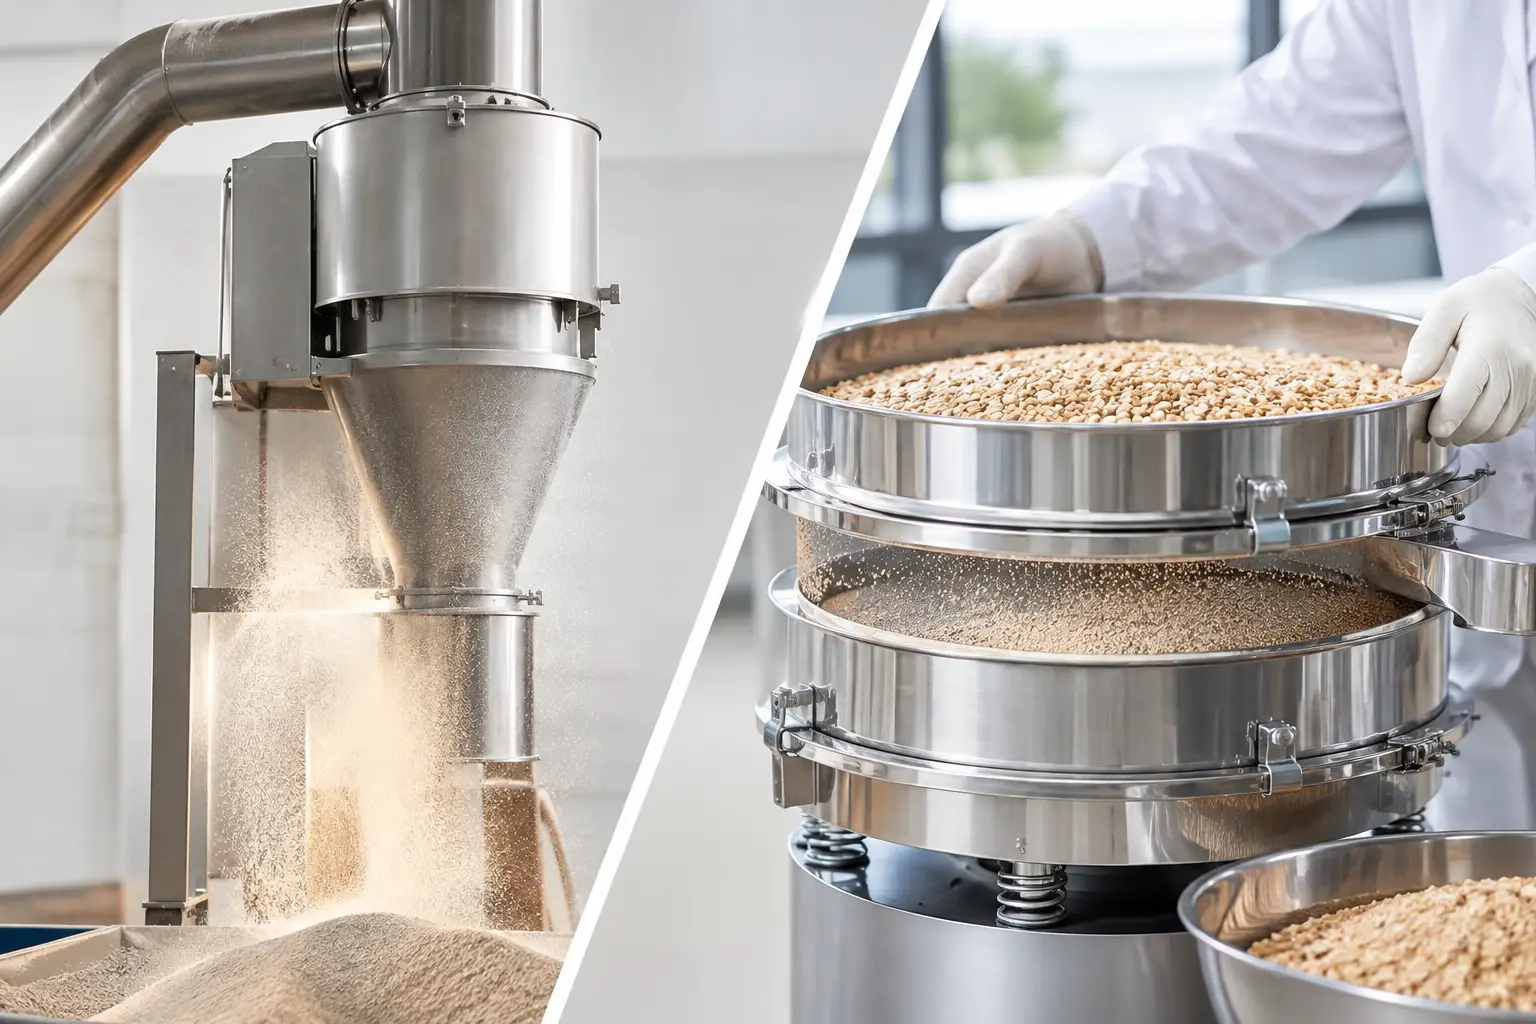
The first task is to identify the assets whose failure has disproportionate consequences. On a powder handling line, that may include the main blower, rotary valve, dust collection fan, load cells, screw feeders, and the control hardware coordinating ingredient addition. In a high-viscosity mixing process, critical assets may be the mixer drive, shaft seals, hydraulic power unit, vacuum system, jacket controls, and discharge valve.
Criticality should reflect more than replacement cost. Consider the consequences for operator safety, environmental control, regulatory compliance, product quality, downtime duration, spare-part lead time, and recovery after an interruption. A relatively inexpensive sensor on a feeder can be more valuable than extensive monitoring on a noncritical auxiliary motor if that feeder governs batch accuracy.
This is also where line-level thinking matters. A machine can be mechanically healthy yet create production risk because it is operating outside its intended process envelope. Repeated high-torque events on an extruder, for example, may indicate formulation variation, poor upstream feeding, temperature-control limitations, or worn mechanical components. The maintenance signal must be interpreted with the process signal.
Build a Condition Baseline Before Setting Alarms
Predictive maintenance depends on knowing what normal operation looks like. That baseline should be established during stable production across expected product types, batch sizes, and operating rates. One fixed alarm limit rarely fits every material or recipe.
For rotating equipment, vibration, temperature, motor current, speed, and lubrication condition can reveal developing bearing, alignment, imbalance, or load problems. For pneumatic systems, useful indicators may include conveying pressure, air velocity, blower current, filter differential pressure, and cycle time. In automated dosing systems, weight deviation, refill time, feeder torque, and control correction frequency can expose loss of performance.
The most useful condition indicators are those that connect directly to a known failure mode. Monitoring gearbox temperature is useful when temperature rise has a credible relationship to lubrication breakdown, overload, or internal wear. Monitoring every available tag because it exists can obscure the signals that operators and reliability teams actually need.
Baseline development also requires disciplined data context. A rise in mixer motor current may be expected when processing a denser formulation or operating at a higher fill level. Without recipe, throughput, temperature, and operating-state data, the same reading can be interpreted incorrectly. Controls architecture should make it possible to distinguish startup from steady-state operation, cleaning from production, and one product campaign from another.
Combine Equipment Data With Process Performance
The strongest predictive maintenance programs do not separate maintenance history from production history. They connect alarms, work orders, inspection findings, and component replacements with process trends and finished-product results.
Consider a milling system producing a tighter particle-size specification. If mill amperage rises gradually while throughput falls and sieve results begin trending toward the upper limit, the issue may be wear, screen blockage, feed inconsistency, or an air-classification change. Maintenance can investigate before the line produces unacceptable material or reaches a forced shutdown.
The same principle applies to liquid and paste processing. A gradual increase in homogenizer pressure at a constant flow rate may point to wear, restriction, viscosity changes, or a control issue. The response should not be an automatic component replacement. It should be a structured review of the equipment condition, formulation, operating parameters, and recent maintenance actions.
This distinction matters because false positives erode trust. If every deviation produces an urgent alert, operators learn to disregard alerts. Predictive maintenance should prioritize actionable exceptions: conditions that have a defined owner, a reasonable diagnostic path, and a clear decision on whether to continue operating, inspect during the next planned window, or intervene immediately.
Design the Workflow Around Decisions
Condition monitoring has limited value if no one owns the response. A practical workflow assigns responsibility from detection through verification. Controls systems may identify the deviation, but maintenance personnel need access to the trend, process engineers need to understand production context, and operations must determine whether a planned intervention fits the schedule.
For each critical condition, define the decision criteria in advance. A moderate vibration increase on a redundant transfer fan may justify closer monitoring and a scheduled inspection. The same increase on a single fan serving a dust-control system may require immediate action because the safety and production consequences are different.
Work orders should capture what was found, what was corrected, and whether the predicted failure mode was confirmed. Over time, that feedback improves alarm thresholds and inspection intervals. It also identifies recurring design issues, such as a component that fails because of poor access, inadequate sealing, material buildup, or operation outside the equipment’s intended duty.
Spare-parts planning belongs in this workflow. Predictive insight is most useful when it creates time to source a critical gearbox, seal kit, drive, or control component before failure. For long-lead items, condition trends can support a controlled procurement decision instead of an emergency purchase made under production pressure.
Predictive Maintenance for Process Lines Requires Integration
A line is only as predictable as the data and responsibilities connecting its systems. Standalone equipment may have local diagnostics, while plant historians, supervisory controls, maintenance management systems, laboratory records, and operator logs hold the rest of the story. The goal is not necessarily to place all data in one platform. The goal is to ensure the relevant teams can see enough context to make a sound decision.
Integration must also account for validation and change-control requirements. Pharmaceutical, food, and other controlled environments may require documented approval before modifying alarm logic, sensor configurations, data handling, or maintenance procedures. Cybersecurity, network reliability, and data ownership should be addressed early, especially when remote access or cloud-based analytics are under consideration.
For new capital projects, predictive capability is easiest to establish during line design. Equipment access, sensor locations, wiring, controls standards, historian tags, and maintenance data structures can be specified before installation. For existing lines, a phased approach is often more practical: begin with one high-consequence process area, prove the workflow, then expand based on measurable results.
Proc-X approaches this work as a process integration issue, not an isolated equipment feature. The useful question is whether the maintenance strategy supports consistent material handling, processing, and finished-product performance across the entire line.
Measure Value Beyond Avoided Downtime
Avoided breakdowns are visible, but they are not the only measure of success. A mature program can reduce unplanned maintenance, improve schedule adherence, extend useful component life, stabilize throughput, reduce scrap, and improve confidence in production commitments. In applications with expensive ingredients or strict specifications, preventing one compromised batch may justify the effort.
Results should be measured against the original risk. If the program was intended to protect blend uniformity, track quality deviations and batch holds alongside maintenance indicators. If it was intended to reduce pneumatic conveying interruptions, monitor line availability, blockage events, energy use, and response time. A condition-monitoring project that generates impressive dashboards but does not change maintenance or operating decisions has not yet delivered its full value.
The right starting point is usually one process constraint that the plant cannot afford to ignore. Instrument it with purpose, establish normal performance, assign a response path, and use the findings to make the next maintenance decision more certain.