A stable emulsion is not created by horsepower alone. A formulation may look acceptable at pilot scale, then separate in a tote, develop an unacceptable droplet-size distribution, or lose throughput once production conditions change. Selecting among industrial emulsifier options requires matching the equipment’s energy input, flow pattern, and residence time to the material system – not selecting a machine based on speed or capacity in isolation.
For process engineers and project teams, the decision affects product quality, batch time, cleanability, utilities, maintenance exposure, and the ability to scale a process without reformulation. The right system creates a controlled, repeatable dispersion. The wrong one can introduce air, excessive heat, particle damage, or an emulsion that is only stable long enough to pass an initial inspection.
What an Industrial Emulsifier Must Accomplish
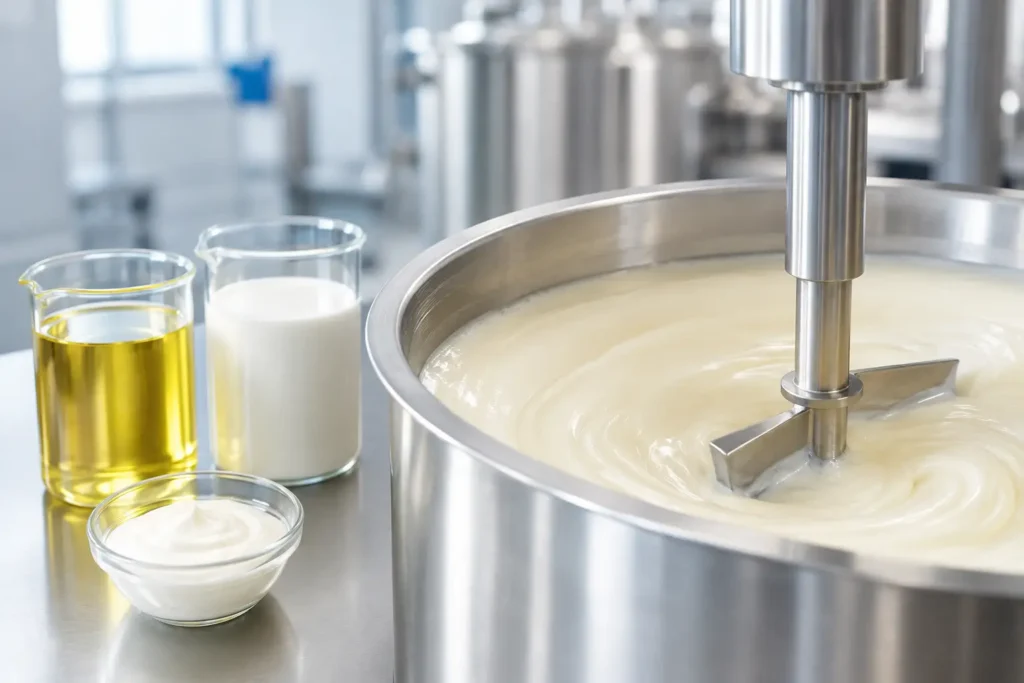
Emulsification reduces one liquid phase into fine droplets and distributes those droplets through another immiscible phase. In many manufacturing applications, the objective extends beyond simple visual uniformity. The process may need to achieve a defined droplet-size range, activate stabilizers, wet powders without fisheyes, disperse waxes or gums, or create a texture and viscosity that remain consistent through filling and storage.
The governing variables are interdependent. Higher shear can reduce droplet size, but it can also raise product temperature and damage shear-sensitive components. More recirculation can improve uniformity, but it adds processing time and may increase air entrainment if the vessel, pump, and return geometry are not designed correctly. An emulsifier should therefore be evaluated as part of the full process system, including ingredient addition, heating or cooling, vacuum capability, transfer, controls, and downstream packaging.
Industrial Emulsifier Options by Process Requirement
The most appropriate equipment category depends on formulation behavior, target capacity, viscosity profile, sanitation requirements, and whether the process is batch, continuous, or hybrid. Several technologies can produce emulsions, but they do not produce the same result or operate under the same constraints.
Batch rotor-stator emulsifiers
A batch rotor-stator unit applies high mechanical shear in a localized workhead zone. Material is drawn into the rotor-stator assembly, accelerated, and forced through openings in the stator. This action is effective for liquid-liquid emulsions, powder incorporation, and dispersion of many thickeners, pigments, and functional ingredients.
Batch systems are often suitable when formulations change frequently, production volumes are moderate, or the process requires staged additions. A vessel-mounted high-shear mixer can be combined with an anchor agitator or sweep mixer for bulk movement, wall heat transfer, and management of increasing viscosity. The high-shear head develops the emulsion while the low-speed agitator keeps the entire batch moving through the working zone.
This arrangement is flexible, but process time can increase as viscosity rises. Dead zones, vessel geometry, and liquid level matter. A high-shear mixer cannot correct poor bulk circulation in a large or poorly configured vessel.
Inline high-shear emulsifiers
Inline rotor-stator emulsifiers process material through a fixed shear zone as it moves through a pipe loop or continuous line. They are well suited to high-throughput production, recirculation processing, and processes that benefit from controlled repeat passes through the workhead.
For a recirculation system, the design must account for pump selection, loop volume, pressure drop, return location, and the number of passes required to reach specification. A single pass may be enough for one formulation and insufficient for another. When product quality depends on a narrow particle or droplet-size distribution, residence time and pass control should be designed into the automation strategy rather than left to operator judgment.
Inline equipment can reduce batch processing time and support more consistent results, particularly when paired with controlled feeding and automated temperature management. It is less forgiving when upstream addition is inconsistent. Powder agglomerates or poorly premixed phases can limit final performance regardless of downstream shear.
Colloid mills
Colloid mills create intense shear through a narrow, adjustable gap between a rotor and stator. They are commonly used when a fine, repeatable dispersion is needed in products ranging from food emulsions and sauces to cosmetic creams, chemical slurries, and specialty pastes.
The adjustable gap gives process teams a direct operating variable, but it also creates trade-offs. Tighter settings generally increase shear and pressure demand while raising the risk of heat generation and wear, particularly with abrasive solids. A colloid mill may be an effective finishing step after bulk mixing, rather than the sole device used to incorporate all ingredients.
Maintenance planning is essential. Wear changes the process gap, which can change product performance. For abrasive, hard, or mineral-filled formulations, material selection and inspection intervals should be addressed during equipment specification.
High-pressure homogenizers
High-pressure homogenizers force product through a restrictive valve or interaction chamber at elevated pressure. The resulting pressure drop, turbulence, cavitation, and impact can produce very fine droplets and dispersions. These systems are used where tight droplet-size control or highly stable emulsions are critical, including selected food, pharmaceutical, nutraceutical, and personal-care applications.
Their performance comes with operational requirements. Feed material must be sufficiently uniform and free of oversized particles that could plug or damage the homogenizing valve. Pressure-rated piping, upstream pumping, cooling capacity, clean-in-place requirements, and maintenance access must all be included in the project scope. High-pressure homogenization is not automatically the correct choice for a viscous product or a formulation with large solids.
Vacuum emulsifying systems
Vacuum emulsifying systems combine agitation, high shear, and vacuum processing in a closed vessel. They are especially valuable for creams, ointments, gels, sauces, and other products where air removal, ingredient wetting, and controlled heating or cooling are part of the process objective.
Vacuum can reduce entrained air, improve powder drawdown, and support a smoother finished appearance. It can also assist with deaeration before filling. However, vacuum does not replace correct agitation or high-shear design. The vessel needs sufficient bulk turnover, appropriate workhead placement, and a process sequence that accounts for when vacuum is applied relative to powder addition, heating, and emulsification.
Selection Criteria That Change the Equipment Decision
A credible equipment specification begins with the formulation and required finished-product performance. Teams should establish the dispersed-phase volume, continuous-phase viscosity, target droplet-size range, solids loading, temperature limits, and whether the product changes viscosity during processing. A low-viscosity oil-in-water emulsion and a high-solids topical cream may both be described as emulsions, yet they can require fundamentally different process arrangements.
The following factors typically determine which option is viable:
- Viscosity across the entire batch cycle: Select for the highest expected process viscosity, not the initial liquid state. Bulk agitation and pumping capability often become the limiting factors.
- Required particle or droplet-size distribution: Visual appearance is not a sufficient acceptance criterion when stability, texture, release behavior, or downstream filling performance depends on distribution.
- Thermal sensitivity: High shear and recirculation generate heat. Products containing volatile flavors, active ingredients, proteins, or temperature-sensitive polymers may require jacket cooling, short residence time, or a different shear strategy.
- Sanitation and validation requirements: Hygienic finishes, drainability, clean-in-place coverage, material traceability, and validation documentation should be designed into the system rather than added after installation.
- Production operating model: Frequent changeovers favor flexible batch systems. High-volume, stable formulations may justify continuous or inline processing with automated control.
Scale-up deserves particular attention. Tip speed alone is not a complete scale-up criterion. The process team should consider power per unit volume, circulation rate, shear-zone exposure, vessel proportions, addition rate, and the effect of hold time before filling. Pilot trials are most valuable when they measure the attributes that define commercial success, such as droplet size, viscosity, air content, stability, and batch-to-batch repeatability.
Design the Emulsification System, Not Just the Machine
An emulsifier performs within a larger production environment. Upstream raw-material handling determines whether powders arrive consistently and whether liquids are dosed accurately. Temperature control affects viscosity and phase behavior. Transfer equipment must move the product without destabilizing it, while filling equipment must handle the finished viscosity and any remaining entrained air.
Controls are equally significant. Recipe-driven sequencing can control phase additions, agitation speeds, vacuum level, temperature ramps, recirculation duration, and end-point criteria. Instrumentation for temperature, pressure, flow, load cells, and motor current can provide useful evidence that each batch followed the intended process. For regulated or high-value products, this process data supports quality investigations and repeatable scale-up.
Proc-X approaches emulsification as an integrated processing requirement: one engineering standard across material handling, mixing, high-shear processing, thermal control, automation, and downstream integration. That approach reduces the risk of designing a capable emulsifier into an incapable overall line.
The practical next step is to define what “stable” means for the product under real production conditions. When the acceptance criteria, formulation behavior, and operating constraints are clear, the best emulsification technology becomes an engineering decision rather than a catalog comparison.