A feeder that holds its rate at startup but slowly moves off target during a production run creates a problem larger than a missed setpoint. Feeder drift causes can affect formulation accuracy, batch uniformity, yield, traceability, downstream equipment loading, and compliance. In continuous or semi-continuous processes, small errors accumulated over hours can become a significant material balance discrepancy.
Drift is not a single failure mode. It is a symptom that must be separated from normal short-term variation. The correct response is not to immediately retune the controller or replace a load cell. It is to determine whether the deviation originates in the material, feeder mechanics, weighing system, controls, or the equipment surrounding the feeder.
What Feeder Drift Actually Looks Like
A true drift condition is a sustained change between the commanded feed rate and the actual delivered rate. It may appear as a gradual loss of rate as a hopper empties, a steady increase in delivery after equipment warms up, or a recurring offset after refill. The feeder can be volumetric, loss-in-weight, gain-in-weight, or part of a larger automated dosing system, but the diagnostic principle is the same: identify what changed as the process ran.
Short-term rate fluctuation is different. A feeder handling a cohesive powder may cycle around its target because material is intermittently entering the screw. That behavior may require mechanical or control improvements, but it is not necessarily drift. Drift is directional and persistent. Distinguishing the two prevents teams from applying the wrong corrective action.
Material Behavior Is a Common Source of Feeder Drift Causes
Bulk solids do not behave like an ideal, uniform fluid. A powder that performed well in a short equipment trial can change behavior over a full shift as its moisture, temperature, particle distribution, or consolidation state changes.
Bulk density changes
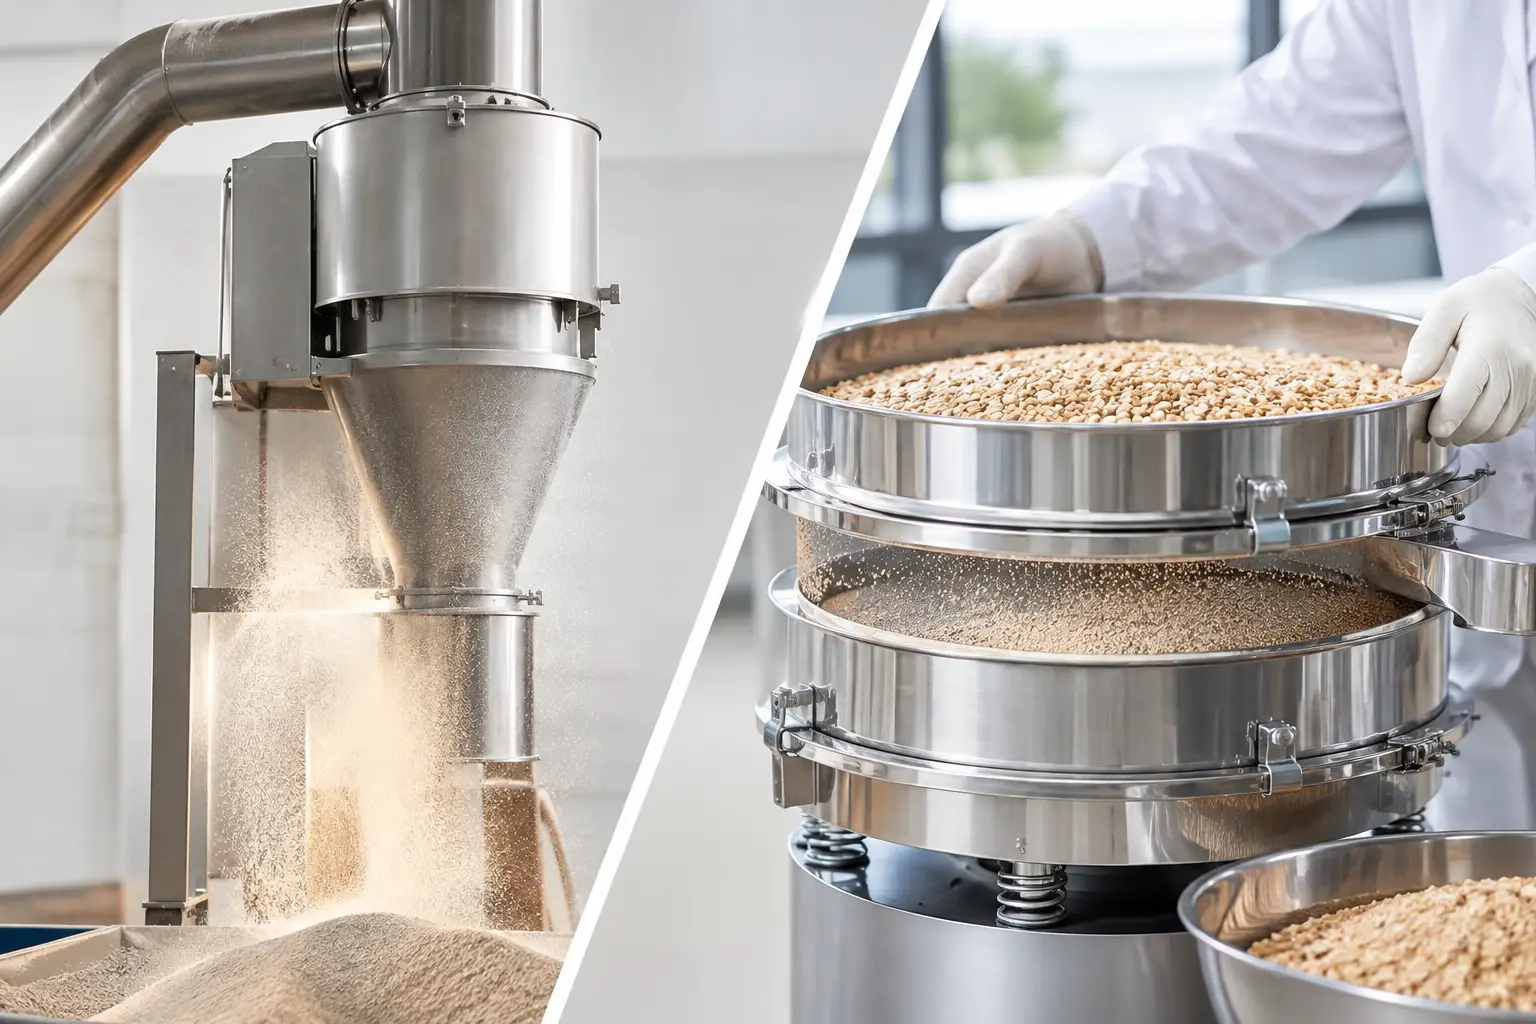
Volumetric feeders are especially sensitive to bulk density. If screw speed remains constant while the material becomes more aerated, compacted, or segregated, mass throughput changes. Even a gravimetric feeder can be affected indirectly when density variation changes screw fill, refill behavior, or the consistency of material entering the metering zone.
Density changes often occur after pneumatic conveying, during hopper refill, or when fine material compacts under head pressure. Materials with a broad particle-size distribution may segregate in hoppers and intermediate bins, causing the feed screw to see a different material fraction over time. The feeder may be mechanically sound while the process upstream is creating the instability.
Moisture, temperature, and time at rest
Hygroscopic powders can absorb moisture and become more cohesive during production. Fat-containing ingredients can soften as ambient or process temperatures rise. Some materials gain strength while stored at rest, then release inconsistently once agitation begins. These changes alter wall friction, internal friction, screw fill, and discharge behavior.
The question is not simply whether the material is labeled free-flowing. It is whether its flow properties remain stable across the actual operating window, including dwell time, refill frequency, plant humidity, and material temperature. A feeder selected for one material state may drift when the product condition changes.
Bridging, rat-holing, and inconsistent hopper discharge
A feeder cannot deliver a stable mass flow if the hopper does not present material consistently to the metering device. Bridging interrupts material supply. Rat-holing allows flow through a narrow channel while stagnant material remains against the hopper walls. Both conditions can produce apparent drift as screw fill decreases or changes unpredictably.
Agitation, flexible hopper walls, live-bottom devices, flow aids, and hopper geometry can help, but each introduces trade-offs. Excessive agitation may compact friable powders, separate blends, generate fines, or create unnecessary load-cell disturbance. The material and desired finished-product quality must guide the solution.
Mechanical Conditions That Change Delivered Rate
Mechanical feeder drift often develops gradually, which makes it easy to overlook during routine inspections. Wear, alignment, and buildup should be evaluated under operating conditions, not only during shutdown.
A worn screw, auger tube, rotary valve, or agitator can reduce metering consistency. Abrasive materials may enlarge clearances and increase internal recirculation. Sticky products may accumulate on screws or in discharge transitions, changing the effective geometry of the metering system. A small deposit can become a growing process restriction if cleaning access and inspection intervals are not aligned with the material.
Drive performance also matters. A gearbox with backlash, a slipping belt, an incorrectly sized motor, or a variable-frequency drive with unstable low-speed control can create rate error that appears to be a material issue. Verify actual shaft speed and torque trends rather than relying only on the speed command shown in the control system.
Hopper and feeder mounting deserve the same attention. If a feeder is mounted on load cells, mechanical interference from guards, flexible connections, conduit, product buildup, or support steel can distort the measured weight loss. These conditions may be intermittent, particularly when adjacent equipment vibrates or thermal expansion shifts connected piping.
Weighing-System Errors Can Mimic Process Drift
Loss-in-weight feeders calculate rate from a changing weight signal. That makes load-cell integrity, signal quality, and mechanical isolation central to accuracy. A stable display does not prove that the weighing system is performing correctly at production rates.
Load cells can be affected by side loading, cable damage, moisture ingress, temperature shifts, poor grounding, and calibration drift. Signal filtering can also create problems. Too little filtering allows vibration to dominate the calculated rate. Too much filtering delays the response and can cause the controller to correct after the process has already moved away from target.
Refill is another critical point. During refill, a loss-in-weight feeder typically operates in volumetric mode because the weight signal is temporarily disturbed. If the volumetric refill rate is not properly characterized, or if refill changes material aeration and screw fill, the feeder may return to gravimetric control with a repeated offset. Trending rate error before, during, and after refill often reveals whether the problem is tied to material replenishment.
Calibration should be verified with a disciplined method that reflects the installed system. A static test-weight check is useful, but it does not expose dynamic errors from vibration, interference, or control filtering. Compare feeder totals against an independent, traceable mass measurement over a representative run whenever process requirements warrant it.
Controls and Integration Can Create the Wrong Correction
Control tuning is frequently blamed for drift because the symptom appears on a trend screen. Yet tuning cannot correct a feeder that is intermittently starved, mechanically binding, or receiving an invalid weight signal. Controls should be addressed after the material path and mechanical condition have been confirmed.
A poorly tuned rate controller may overcorrect after normal material disturbances. Aggressive gain can cause cycling, while conservative tuning may allow a slow offset to persist too long. The appropriate response depends on feeder size, material response time, filtering, refill strategy, and the sensitivity of the downstream process.
System integration can introduce hidden constraints. A pneumatic transfer line may pull on a feeder outlet. A common dust-collection connection can impose a pressure change. A downstream mixer, extruder, or conveyor may create pressure, torque, or level feedback that changes discharge conditions. Treating the feeder as an isolated machine can miss the physical interaction causing the rate change.
A Practical Method for Diagnosing Feeder Drift Causes
Start with a time-based production trend, not a single observation. Plot commanded rate, calculated actual rate, screw speed, hopper weight, refill events, motor torque where available, and relevant upstream or downstream signals. Then ask what event consistently precedes the deviation.
A disciplined investigation typically follows four steps:
- Confirm the error with an independent mass check over a meaningful run length. This separates a true delivery issue from a display or calculation issue.
- Inspect material condition and flow at the feeder inlet. Look for changes in bulk density, bridging, segregation, level-dependent behavior, and refill-related aeration.
- Examine the mechanical system while operating. Check screw fill, buildup, wear, drive speed, vibration, flexible connections, and any contact points around the weighing frame.
- Review the weighing and control logic after the physical system is understood. Verify calibration, signal stability, filtering, refill transitions, and controller response.
This sequence reduces wasted effort. Adjusting parameters before confirming the material path often masks the evidence needed to find the real cause.
Corrective Action Should Address the Process, Not Only the Feeder
The right correction may be as simple as eliminating a load-cell interference point or as involved as redesigning the hopper-to-feeder transition. For difficult materials, stable feeding may require a coordinated package of hopper geometry, agitation, screw design, refill strategy, containment, and controls. The objective is repeatable material presentation at the metering element, not merely a feeder that passes a short acceptance test.
Proc-X approaches feeding accuracy as part of the production system. Material characteristics, operating environment, required rate range, cleaning expectations, automation architecture, and downstream process demand all influence the engineered solution. One feeder may be appropriate for a free-flowing mineral powder and entirely unsuitable for a cohesive nutraceutical blend or abrasive battery material.
When drift is investigated with measured data and a full-system view, corrective actions become more durable. The most useful next step is to capture a representative production trend before the next adjustment, then let the evidence identify where the process is losing control.