A production line can be mechanically complete and still be unready to make saleable product. Process equipment commissioning is the disciplined transition from installed assets to a controlled, repeatable operating system – one that handles the actual material, reaches the required rate, protects product quality, and gives operators confidence in normal and abnormal conditions.
For powder, liquid, paste, and high-viscosity processing systems, this distinction matters. A feeder can rotate, a mixer can run, and a packaging machine can cycle without proving that the full line will maintain dosing accuracy, blend uniformity, particle integrity, transfer reliability, or batch traceability. Commissioning establishes that proof before startup pressure turns unresolved details into production losses.
Process Equipment Commissioning Is a System Activity
Commissioning is often treated as the final project phase after fabrication, installation, and electrical completion. That view is incomplete. The work begins much earlier, when the project team defines what the process must accomplish and how performance will be measured.
An individual machine may meet its mechanical specification while the integrated process fails to meet its production objective. A pneumatic conveying system may move material successfully but create fines. A high-shear mixer may achieve dispersion but introduce unacceptable heat. A loss-in-weight feeder may hold accuracy in a short static test yet drift during refill cycles, vibration, or changing bulk density. These are system-level outcomes, and they require system-level commissioning.
The commissioning scope should therefore connect equipment operation to the approved process basis: material properties, target throughput, batch size, recipe sequence, cleaning requirements, utility conditions, safety functions, data requirements, and finished-product specifications. It also needs defined ownership. When equipment suppliers, controls contractors, installers, and plant personnel test isolated portions of the line without one coordinated plan, gaps tend to appear at the interfaces.
For integrated projects, one engineering standard and one point of accountability reduce that risk. The goal is not merely to complete a punch list. It is to demonstrate that the installed line performs as the process was intended to perform.
Start With Conditions the Equipment Will Actually See
The most useful commissioning plans are built around real operating conditions, not idealized demonstrations. That means testing with representative materials whenever practical and accounting for the variability that production will encounter.
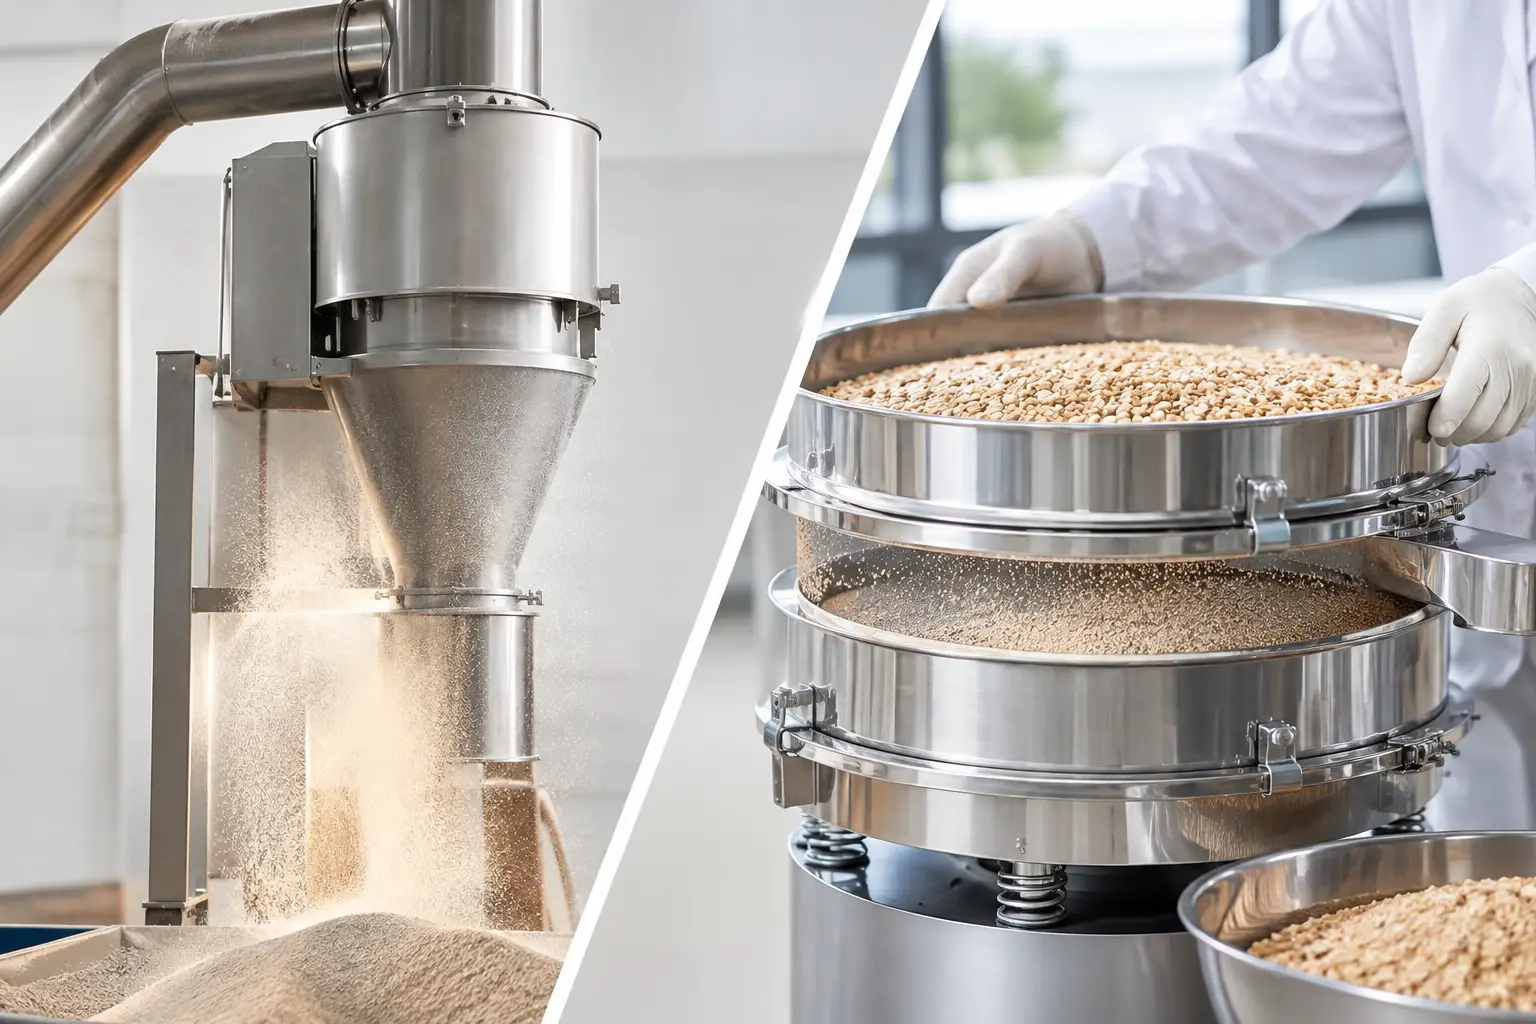
For dry materials, bulk density, moisture, particle-size distribution, flowability, electrostatic behavior, and friability can all affect results. A system commissioned with a free-flowing surrogate may not reveal bridging in a hopper, rat-holing above a screw feeder, dust escape at a transfer point, or segregation during conveying. In wet and viscous processes, viscosity curves, temperature, entrained air, shear sensitivity, and cleaning chemistry can change both equipment performance and final-product quality.
This does not mean every project must wait for full-scale product trials. In pharmaceutical, defense, specialty chemical, and emerging-material applications, product availability, cost, or handling restrictions may limit what can be used. In those cases, the engineering team should select a surrogate with known limits and document which process conditions still require site acceptance or qualification testing. The key is to avoid treating a surrogate result as a complete product-performance guarantee.
Define Acceptance Criteria Before Testing Begins
Commissioning becomes inefficient when success is defined after a test has already been run. Clear acceptance criteria give the project team a common decision framework and prevent subjective signoff.
Criteria should be specific to the application. A bulk solids system might be evaluated for feed-rate stability, transfer rate, dust containment, material residuals, and particle degradation. A blending system may require evidence of uniformity within a stated sampling plan. A liquid processing skid may need to demonstrate temperature control, pressure stability, emulsification performance, and cleanability. An automated line may be judged on recipe execution, alarm response, electronic records, interlocks, and data transfer to plant systems.
Not every requirement carries the same weight. Some are safety-critical, some are quality-critical, and others affect operating efficiency or maintainability. Categorizing requirements helps the team resolve deviations in the right order. A guard interlock failure and a nonessential label format issue should not receive the same commissioning priority.
The Commissioning Sequence That Reduces Startup Risk
A structured sequence avoids the common mistake of attempting full production before basic functions have been proven. The exact order depends on the process, but the progression should move from safe static verification to controlled dynamic operation.
Verify Mechanical, Utility, and Safety Readiness
Before material enters the process, confirm that the installed equipment matches approved drawings and that all required utilities are available at the correct conditions. This includes electrical supply, grounding, compressed air quality and pressure, vacuum capacity, process water, thermal media, dust collection, exhaust, and drainage where applicable.
Mechanical checks should address more than rotation and alignment. Inspect access for cleaning and maintenance, gasket compatibility, sanitary connections, instrument installation, support stiffness, guarding, lubrication, and the integrity of product-contact surfaces. In abrasive applications, verify wear components and access points before operation makes later inspection difficult.
Safety verification is equally fundamental. Emergency stops, permissives, pressure relief, dust hazard controls, machine guarding, lockout provisions, and alarm annunciation must function as designed. A process cannot be considered commissioned if it produces acceptable material but exposes personnel or equipment to avoidable risk.
Prove Controls Before Full-Rate Production
Controls commissioning confirms that the equipment responds correctly to commands, instruments provide credible feedback, and the process moves through its intended sequence. Input/output checks are necessary, but they are not sufficient. The team must test cause-and-effect logic, permissives, interlocks, failure modes, alarm priorities, recovery sequences, and manual operating functions.
For example, a batching system should be tested through normal dosing, feeder refill, out-of-tolerance correction, aborted batches, power interruptions, and operator intervention. A thermal process should be tested for sensor failure, high-temperature response, and controlled shutdown. For regulated operations, user access, audit trails, recipe control, and electronic records may be as important as motor logic.
Operators should participate at this stage, not only after turnover. Their feedback often identifies unclear human-machine interface screens, impractical alarm messages, poor access arrangements, or recovery steps that are technically valid but operationally unrealistic.
Run Material Through the Entire Process
Integrated material trials are where hidden dependencies become visible. Feed behavior affects transfer. Transfer behavior affects weighing. Weighing affects mix consistency. Mixing affects downstream drying, extrusion, filling, or packaging. A line must be assessed as a connected production system rather than a set of commissioned machines.
Testing should include expected operating ranges, not only the nominal setpoint. Run lower and higher rates where relevant, evaluate recipe changes, observe startup and shutdown losses, and assess the effect of refill cycles or upstream interruptions. If the process is continuous, confirm stable operation over enough time to reveal drift, buildup, heat accumulation, or control instability. If it is batch-based, assess repeatability across multiple batches.
The trade-off is practical: extensive trials take time and consume material, but compressed testing can leave the plant to discover predictable issues during commercial production. The right depth depends on process risk, product value, regulatory exposure, and the cost of lost capacity after startup.
Documentation Turns Tests Into an Operating Asset
Commissioning documentation is often seen as project closeout paperwork. Done well, it becomes the foundation for operations, maintenance, validation, and future process improvement.
A complete record should show what was tested, under which conditions, what results were obtained, what deviations occurred, and how those deviations were resolved or accepted. It should also capture final equipment settings, control parameters, calibration status, approved recipes, spare-parts recommendations, maintenance requirements, and operator training completion.
This record matters when production is scaled, a new formulation is introduced, or a later performance issue must be investigated. Without a reliable baseline, teams spend time debating what the system originally demonstrated instead of diagnosing the current condition.
For regulated manufacturing, the relationship between commissioning, qualification, and validation must be planned carefully. Commissioning demonstrates that the equipment and controls operate as engineered. Qualification and validation may require additional documented evidence that the system consistently meets intended use and product requirements. The boundaries vary by industry and internal quality system, but the activities should be coordinated rather than duplicated.
Common Gaps That Delay Productive Startup
Most commissioning delays are not caused by a single catastrophic defect. They result from small unresolved issues that compound across disciplines. Incomplete utility capacity, uncalibrated instruments, missing control narratives, late recipe decisions, unclear ownership of interfaces, and unavailable production materials can each hold up a line that appears nearly finished.
Another recurring problem is treating training as a handoff event. Operators and maintenance personnel need practical familiarity with startup, shutdown, cleaning, troubleshooting, changeover, and safe recovery from faults. The best time to build that competence is during supervised commissioning, when engineers, controls specialists, and equipment experts are still available to explain why the system behaves as it does.
Proc-X approaches commissioning with the same application-specific discipline used to engineer the process itself. Material behavior, equipment interaction, automation logic, and production objectives must align before the line is asked to carry commercial demand.
A successful startup is not the moment equipment first runs. It is the point at which the plant can run it deliberately, safely, and repeatedly with a clear standard for what good performance looks like.